

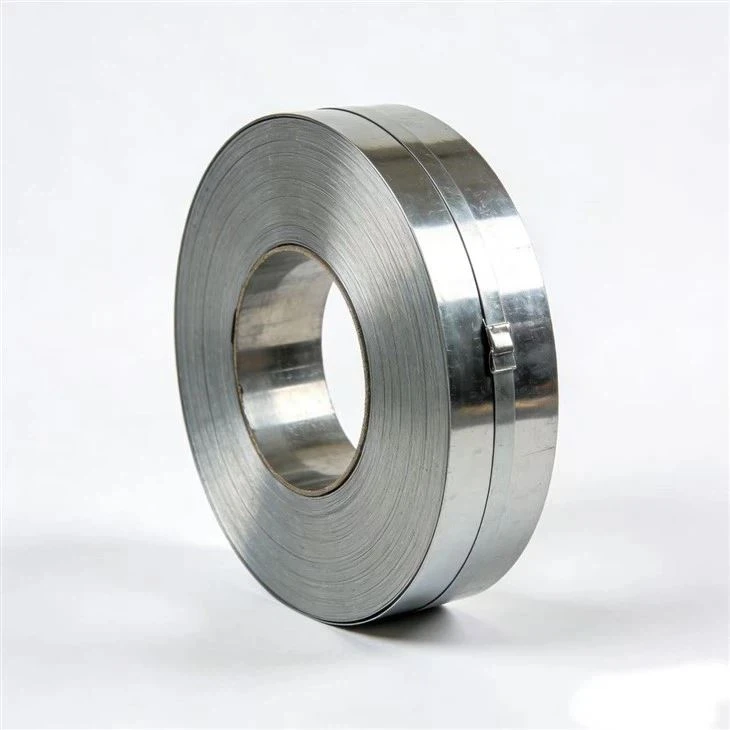
Precision-rolled spring steel strip engineered for applications demanding high yield strength, fatigue resistance, and controlled elastic recovery. Supplied in cold-rolled annealed, hardened, and tempered conditions, these strips maintain strict dimensional tolerances and flat cross-sections suitable for high-speed stamping, fine blanking, roll forming, and spring coiling.
Key Product Characteristics
High Yield Ratio (Rp0.2 / Rm): Exceeds 0.85 in hardened/tempered condition, preventing permanent set under cyclic loading.
Tight Gauge Uniformity: Thickness tolerances down to +/-0.005 mm minimize punch wear and maintain consistent spring rate (k).
Controlled Surface Decarburization: Maximum total decarburization depth bounded under 1.0% of nominal thickness per side to eliminate premature fatigue initiation.
Low Non-Metallic Inclusion Rating: Vacuum-degassed melting practices yield clean steel matrix (ASTM E45 Class A/B thin/heavy < 1.0), ensuring elevated bendability and impact toughness.
Technical Specifications
|
Parameter |
Specification Range |
|
Thickness |
0.05 mm - 6.00 mm |
|
Width |
3.00 mm - 650.00 mm |
|
Thickness Tolerance |
Standard: ISO 9445 Class Normal / Precision: +/-0.005 mm to +/-0.02 mm |
|
Width Tolerance |
Slit Edge: +/-0.10 mm to +/-0.30 mm / Deburred: +/-0.05 mm |
|
Delivery Hardness |
Annealed: <= 210 HV / Hardened & Tempered: 350 - 600 HV (36 - 56 HRC) |
|
Tensile Strength (Rm) |
Annealed: 500 - 700 MPa / Hardened & Tempered: 1100 - 2000 MPa |
|
Edge Profiles |
Mill Edge, Slit (Sheared), Deburred, Rounded (100% radius), Square Cut |
|
Coil ID / OD |
ID: 300 mm, 400 mm, 508 mm / OD: Up to 1400 mm (Oscillated winding available) |
Grades & Standards
|
Standard |
High Carbon Grades |
Alloy Grades |
Corrosion Resistant Grades |
|
EN 10132-4 / EN 10151 |
C55S, C60S, C67S, C75S, C100S |
51CrV4 (1.8159), 80CrV2 (1.2235), 56Si7 |
X10CrNi18-8 (1.4310) |
|
ASTM / AISI |
1055, 1065, 1075, 1095 |
6150, 5160, 9260 |
AISI 301, AISI 304 |
|
JIS G4802 / G4313 |
S55C-CSP, S65C-CSP, SK85-CSP |
SUP6, SUP9, SUP10 |
SUS301-CSP, SUS304-CSP |
Surface & Processing Options
Surface Finishes
- Bright Polished (P): Smooth ground and polished surface (Ra <= 0.3 um) for high fatigue life and low friction.
- Blue Tempered (P+AF): Thermally oxidized uniform blue oxide film providing mild indoor storage corrosion layer.
- Yellow/Gold Tempered: Thermally treated target oxidation for decorative or identification requirements.
- Scaleless Black / Grey (GR): Heat-treated finish without loose oxide scale; suitable for non-critical cosmetic applications.
Temper Conditions
- Cold Rolled + Soft Annealed (+A / G): Spheroidized microstructure (>= 85% spheroidization) optimized for severe cold forming, fine-blanking, and deep drawing prior to secondary heat treatment.
- Hardened & Tempered (+QT / H+A): Quenched and tempered continuous strip ready for blanking, coiling, or forming without subsequent heat treatment.
Applications
Automotive
Clutch diaphragm springs, seat belt retractor springs, valve shim stock, brake pad retaining clips, sensor diaphragms.
Industrial & Electrical
Belleville washers, wave disc springs, cable ties, power tool recoil springs, switch contacts.
Tools & Hardware
Band saw blades, doctor blades, putty knives, feeler gauges, snap rings, circlips.
Quality Control & Inspection
Every production lot undergoes rigorous laboratory verification backed by full traceability from heat number to master coil slitting:
Chemical Analysis: Optical Emission Spectroscopy (OES) verifying heat chemistry limits.
Mechanical Testing: Tensile strength (Rm), yield strength (Rp0.2), elongation (A80), micro-hardness testing (Vickers/Rockwell).
Dimensional Verification: Continuous laser thickness gauge logging along coil length; micro-caliper edge checks.
Microstructure & Surface Inspection: Metallographic verification of grain size, spheroidization rate, decarburization layer, and Eddy Current surface defect detection.
Certification: EN 10204 3.1 Material Test Certificate supplied with each shipment.
Supply & Customization Options
Pancake Coils: Standard single-roll coils wrapped with anti-rust paper and plastic film on wooden skids.
Oscillated / Traverse Wound Coils: Continuous spooling up to 1000 kg per spool, reducing machine downtime during long-run stamping operations.
Cut-to-Length Strips: Flat rectangular sheet strips bundled with steel strapping and edge protectors.
Packaging Protection: VCI (Vapor Corrosion Inhibitor) paper wrapping, sea-freight wooden crates, or heat-treated ISPM-15 compliant pallets.
What Buyers Should Provide for a Quote
To receive a complete technical quotation within 24 hours, include the following parameters in your inquiry:
Steel Grade & Standard: (E.g., C75S per EN 10132-4 or AISI 1075)
Dimensions: Thickness (mm) x Width (mm) x Tolerances (if tighter than standard)
Delivery Condition: Soft Annealed (+A) or Hardened & Tempered (+QT)
Target Hardness / Tensile Strength: (E.g., 42 - 47 HRC or 1300 - 1500 MPa)
Surface Finish & Edge Condition: (E.g., Bright Polished, Slit Edge vs. Rounded Edge)
Coil Configuration & Quantity: Coil weight limits, ID/OD constraints, or cut length; Total tonnage required.
FAQ
Q: What is the difference between soft annealed (+A) and hardened/tempered (+QT) spring steel strips?
A: Soft annealed strip has a spheroidized carbide microstructure with low hardness (<= 210 HV), enabling bending, stamping, and complex forming without tool damage. Parts formed from soft annealed steel must be batch-hardened and tempered afterward. Hardened and tempered strip is continuously heat-treated at the mill to target mechanical properties (35 - 56 HRC), eliminating downstream heat treatment but limiting forming operations to shallow bends or punching.
Q: How do alloy grades like 51CrV4 differ from high-carbon grades like C75S?
A: High-carbon grades (C67S, C75S, C100S) rely primarily on carbon content for hardness and yield strength, making them cost-effective for static or moderate cyclic loading. Alloy grades like 51CrV4 (6150) incorporate Chromium and Vanadium, which refine grain size, increase hardenability, and significantly elevate fatigue strength and elevated-temperature relaxation resistance (up to 300 degrees C).
Q: What edge condition is required to prevent fatigue cracking?
A: Sheared or slit edges contain micro-cracks and work-hardened burrs from the slitting process, which act as stress risers under dynamic bending. For applications undergoing high cyclic stress (such as recoil springs or valve shims), rounded edges (100% radius) or deburred edge profiles are necessary to remove micro-defects and extend fatigue life.
Q: What dimensional tolerances can be maintained across coil lengths?
A: Standard precision cold rolling achieves thickness tolerances of +/-0.008 mm on thin gauges (< 0.50 mm) and up to +/-0.025 mm on thicker strip up to 3.0 mm. Width slitting tolerance is held to +/-0.10 mm under standard setups, with special slitting tooling capable of holding +/-0.05 mm.
Hot Tags: spring steel strip, China spring steel strip manufacturers, suppliers, factory


