Structural Steel & Fabricated Components for Construction Machinery- High-Strength Steel Profiles, Wear-Resistant Plates & Heavy Weldments
Manufacturing high-yield structural steel profiles, wear-resistant steel plates, and precision weldments for excavators, cranes, loaders, and mining equipment. From S690QL and NM400/NM500 steel plates to custom-machined boom sections and chassis components, our products meet EN 10025-6, ASTM A514, and ISO 9001 standards, providing structural stability and fatigue resistance under heavy cyclic loads.
-
![Pickled And Oiled Steel Plate]() Pickled And Oiled Steel PlateName: Pickled and Oiled Steel Plate Suppliers P&O Steel Sheet. Standard: ASTM / EN / JIS / GB Standards. Thickness: 1.5-20mm. Length: Available in Customized Sizes. Delivery Time: 10-25 Working Days.
-
![Hot Rolled Steel Plate Suppliers]() Hot Rolled Steel Plate SuppliersName: Hot Rolled Steel Plate Suppliers Hr Plate Steel. Standard: GB-T / ASTM / EN 10025-6. Thickness: 6-400mm. Length: Customized. Delivery Time: 7-30days. MOQ: 1mt
-
![High Strength Plates]() High Strength PlatesName: High Strength Plates. Standard: GB-T 1591/24186 ASTM A572/A618/A1011 EN 10025-3/4. Thickness: 6-100mm. Length: Customized. Delivery Time: 7-30days. MOQ: 1mt.
-
![Abrasion Resistant Steel Sheet]() Abrasion Resistant Steel SheetName: Abrasion Resistant Steel SheetStandard: GB-T/ASTM/EN 10025Thickness: 5-200mmLength CustomizedDelivery Time: 7-30daysMOQ: 1mt
-
![13CrMo4-5 Heat Resistant Steel Plate – European Standard Low Alloy]() 13CrMo4-5 Heat Resistant Steel Plate – European Standard ...Name: 13CrMo4-5 Heat Resistant Steel Plate – European Standard Low Alloy. Standard: GB-T/ASTM/EN10028-2/ASME. Thickness: 6-250mm. Length Customized. Delivery Time: 7-30days. MOQ: 3mt.
-
![SA387Gr22CL2 Pressure Vessel Steel Plate – ASTM/ASME Standard]() SA387Gr22CL2 Pressure Vessel Steel Plate – ASTM/ASME Stan...Name: SA387Gr22CL2 Pressure Vessel Steel Plate – ASTM/ASME Standard. Standard: GB-T/ASTM/ASTM/ASME. Thickness: 6-300mm. Length Customized. Delivery Time: 7-30days. MOQ: 1mt.
-
![High Carbon Steel Tensile Strength]() High Carbon Steel Tensile StrengthName: High Strength Steel Sheet BS800E. Standard: GB-T/ASTM/EN 10029. Thickness: 2-12mm. Length Customized. Delivery Time: 7-30days. MOQ: 1mt.
-
![Hr Plate Steel]() Hr Plate SteelName: Hr Plate Steel. Standard: GB-T/ASTM/EN 10025-6. Thickness: 6-400mm. Length Customized. Delivery Time: 7-30days. MOQ: 1mt.
-
![Abrasion Plate]() Abrasion PlateName: Wear Resistant Steel Plate NM450Standard: GB-T/ASTM/EN 10025Thickness: 1.8-400mmLength CustomizedDelivery Time: 7-30daysMOQ: 1mt
-
![High Strength Steel Hss]() High Strength Steel HssName: High Strength Steel Hss. Standard: GB-T/ASTM/EN 10029. Thickness: 4-40mm. Length Customized. Delivery Time: 7-30days. MOQ: 1mt.
-
![Asme Sa516 70 Steel Plate]() Asme Sa516 70 Steel PlateName: Asme Sa516 70 Steel Plate. Standard: GB-T/ASTM/EN 10028-2. Thickness: 6-350mm. Length Customized. Delivery Time: 7-30days. MOQ: 1mt.
-
![Asme Sa508 Steel Plate]() Asme Sa508 Steel PlateName: Asme Sa508 Steel Plate. Standard: GB-T/ASTM/EN 10028-2. Thickness: 6-300mm. Length Customized. Delivery Time: 7-30days. MOQ: 1mt.


Product Categories
High-Yield & High-Strength Steel Plates
• Quenched & Tempered Structural Steel: S690QL, S890QL, and Q690D steel plates engineered for mobile crane booms, concrete pump arms, and high-load structural frames.
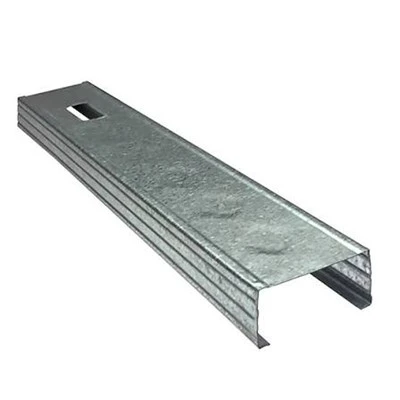
• Heavy-Duty Structural Profiles: Thick-walled C/U channels, welded H-beams, and hollow sections for chassis frames and crawler undercarriages.
Wear-Resistant Steel Solutions
• Abrasion-Resistant Plates (NM400 / NM500 / Hardox Equivalent): High-hardness steel plates (370 to 540 HBW) for excavator buckets, crusher hoppers, and mining truck bed liners.
• Custom Cutting & Curved Liner Plates: CNC flame and plasma cut wear parts pre-drilled and formed for direct field bolt-on or weld-in replacement.
Heavy Fabricated Weldments & Components
• Excavator Boom & Arm Assemblies: Precision-welded structural box sections with ultrasonic-tested full-penetration joints.
• Machined Structural Mounts & Bushings: Heavy steel forgings and thick-plate brackets pre-machined with tight pin-bore tolerances (+/- 0.02 mm).
Technical Specifications
|
Parameter |
High-Yield Structural Steel |
Wear-Resistant Steel |
Fabricated Heavy Weldments |
|
Material Grade |
Q550D, Q690D, S690QL, S890QL, ASTM A514 |
NM400, NM450, NM500, AR400, AR500 |
Q355B, Q690D, S355JR, S690QL |
|
Yield Strength |
550 MPa to 890 MPa |
>= 1000 MPa (Typical) |
According to base steel selection |
|
Tensile Strength |
650 MPa to 1100 MPa |
>= 1250 MPa |
According to base steel selection |
|
Hardness Level |
200 to 280 HBW |
370 to 540 HBW |
N/A (Tested per plate base) |
|
Low-Temp Impact Energy |
>= 30 J at -40 deg C (Charpy V-Notch) |
>= 20 J at -20 deg C |
Tested on weld seams per AWS D1.1 |
|
Plate Thickness Range |
6 mm to 120 mm |
4 mm to 80 mm |
Structural plate thickness up to 150 mm |
|
Machining Tolerance |
Cutting tolerance: +/- 1.0 mm |
Hole positioning: +/- 0.5 mm |
Pin bore diameter: +/- 0.02 mm |
|
Material Standards |
EN 10025-6, GB/T 19879, ASTM A514 |
GB/T 24186, EN ISO 148-1 |
AWS D1.1, EN 1090-2 (EXC Class 3) |

High-Yield Quenched & Tempered Steel (S690QL / Q690D)
• Yield Point: Minimum 690 MPa.
• Key Feature: Low carbon equivalent (CEV <= 0.47%) ensures weldability without cold cracking risk while reducing total structural weight by up to 30% compared to standard S355 steel.
Abrasion-Resistant Steel (NM400 / NM500)
• Hardness: Nominal 400 HBW to 500 HBW across full plate thickness.
• Key Feature: Through-hardened structure resists sliding contact abrasion from quartz, granite, and ore, extending component service life in excavation and material handling.
Weldable Fine-Grain Structural Steel (S355J2+N / Q355D)
• Normalized Condition: Consistent grain structure offering predictable cold forming behavior.
• Key Feature: Ideal balance of toughness and bendability for heavy-duty vehicle chassis and subframes.
Manufacturing & Processing Capabilities
Large-Scale CNC Cutting:
Gantry fiber laser (up to 20 kW) and underwater CNC plasma cutting tables handling plates up to 4.0 meters wide and 18 meters long.
Heavy-Duty CNC Press Braking:
1600-Ton press brake capable of cold-forming high-strength steel up to 25 mm thickness in single-pass lengths up to 12 meters.
Robot & Submerged Arc Welding:
Automated robotic MIG welding stations and heavy submerged arc welding (SAW) units for deep-penetration structural seams.
Post-Weld Machining & Boring:
Floor-type CNC horizontal boring mills achieving bore concentricity within 0.03 mm on large structural fabrications.
Quality Control & Compliance
Ultrasonic Flaw Detection (UT):
100% internal soundless inspection on plate body (ISO 10160 Class S1/E1) and critical weld seams (EN ISO 17640).
Mill Test Certificates (MTC):
Issued per EN 10204 3.1 with every batch, confirming chemical heat analysis, yield strength, tensile tests, and Charpy impact values.
Non-Destructive Testing (NDT):
Magnetic Particle Inspection (MPI) and Dye Penetrant Inspection (DPI) applied to high-stress weld toes and cut edges.
Dimensional & Surface Verification:
Laser tracker dimensional inspection and electronic surface roughness profiling on pre-machined pin joints.
Application Matrix
Excavators & Wheel Loaders:
High-strength boom arms, heavy bucket side-cutters, wear liners, and quick-hitch brackets.
Mobile & Tower Cranes:
Telescopic jib box sections, outrigger beams, and heavy turntable adapter plates.
Mining & Quarry Equipment:
Dump truck bed liners, jaw crusher feed chutes, and conveyor transfer hoppers.
Road & Concrete Machinery:
Concrete pump truck boom sections, paver screed plates, and soil stabilizer mixing drums.
Minimum Order Quantity (MOQ):
• Standard High-Strength Steel Plates: 5 Metric Tons per thickness/grade.
• Custom Cut-to-Size Wear Plates: 10 Pieces.
• OEM Fabricated Weldments / Boom Sections: 2 Units or 3 Metric Tons.
Production Lead Times:
• Standard Cut & Drilled Plates: 10 to 15 days after drawing confirmation.
• Heavy Fabricated Weldments: 25 to 35 days including NDT and trial assembly.
• Monthly Production Capacity: 8500 Metric Tons of heavy structural steel and processed components.

Packaging & Export Logistics
Heavy-Duty Export Packaging:
Steel plates and weldments secured on reinforced heavy-timber runners or steel pallets with heavy steel banding.
Rust Prevention Coating:
Exposed machined surfaces and weld bevels coated with removable anti-rust oil or wax film prior to wrapping.
Container & Break-Bulk Shipping:
Optimized flat-rack (FR), open-top (OT), or standard container loading according to piece dimensions and crane lifting limits at destination ports.
FAQ

Request a Quote
Project Information Required for Estimating
To obtain an accurate quotation and manufacturing schedule, please provide:
Steel Grade & Standard: Required steel designation (e.g., S690QL, NM400, Q355B) and material specification standard.
Component Drawings: CAD files (.dxf, .step, or .pdf) indicating dimensions, tolerances, weld symbols, and machined surfaces.
Quantity & Delivery Schedule: Initial sample requirement, batch quantity, and target delivery timeframe.
Special Quality Requirements: Specific NDT inspection levels (e.g., UT Class, MPI 100%), impact testing temperature, or third-party inspection needs (SGS, BV, TUV).
Contact Heavy Machinery Engineering Team
Email: info@tjrsr.com | Phone / WhatsApp: +86 159 0023 5505
Technical inquiry response time: Within 24 business hours with preliminary engineering review.